Work management
Production guide
Learn how production planning and control works, calculate usable capacity, and connect equipment data and maintenance with the production schedule.
A production plan is only useful if the shop can deliver it. A late material shipment, a machine stop, or an urgent order can change the schedule—and the promises made to customers.
Production planning and control brings those decisions together. It helps teams decide what to make, check the resources required, and respond when the floor runs differently from the plan.
Production planning and control (PPC) is the process of deciding what to produce, when, and with which resources, then monitoring execution and adjusting as conditions change.
Planning turns demand into a schedule for materials, equipment, and people. Control compares actual progress with that schedule, identifies problems, and coordinates the response.
The objective is a plan the plant can execute and a clear way to recover when it cannot.
Production planning connects decisions made at different time horizons. Each level answers a different question:
The levels feed one another. If the capacity check shows a bottleneck or purchasing cannot secure the specified material in time, the master schedule needs a decision—not just a more detailed dispatch list. Maintenance planning identifies the work and resources needed; production and maintenance scheduling agree on an equipment window and allow for return-to-service checks.
A push approach releases work against a schedule or forecast. A pull signal authorizes replenishment in response to actual downstream consumption; a kanban signal is one example. Push gives purchasing visibility for long-lead materials, but a weak forecast can leave excess stock or the wrong work in process. Pull can limit queues, but needs a dependable replenishment process and enough protection against variability.
A duct shop may use both: order coil ahead using the project outlook, then release a manageable batch of fittings when the next operation is ready. The right release size depends on setup time, due dates, available space, and the customer's delivery sequence.
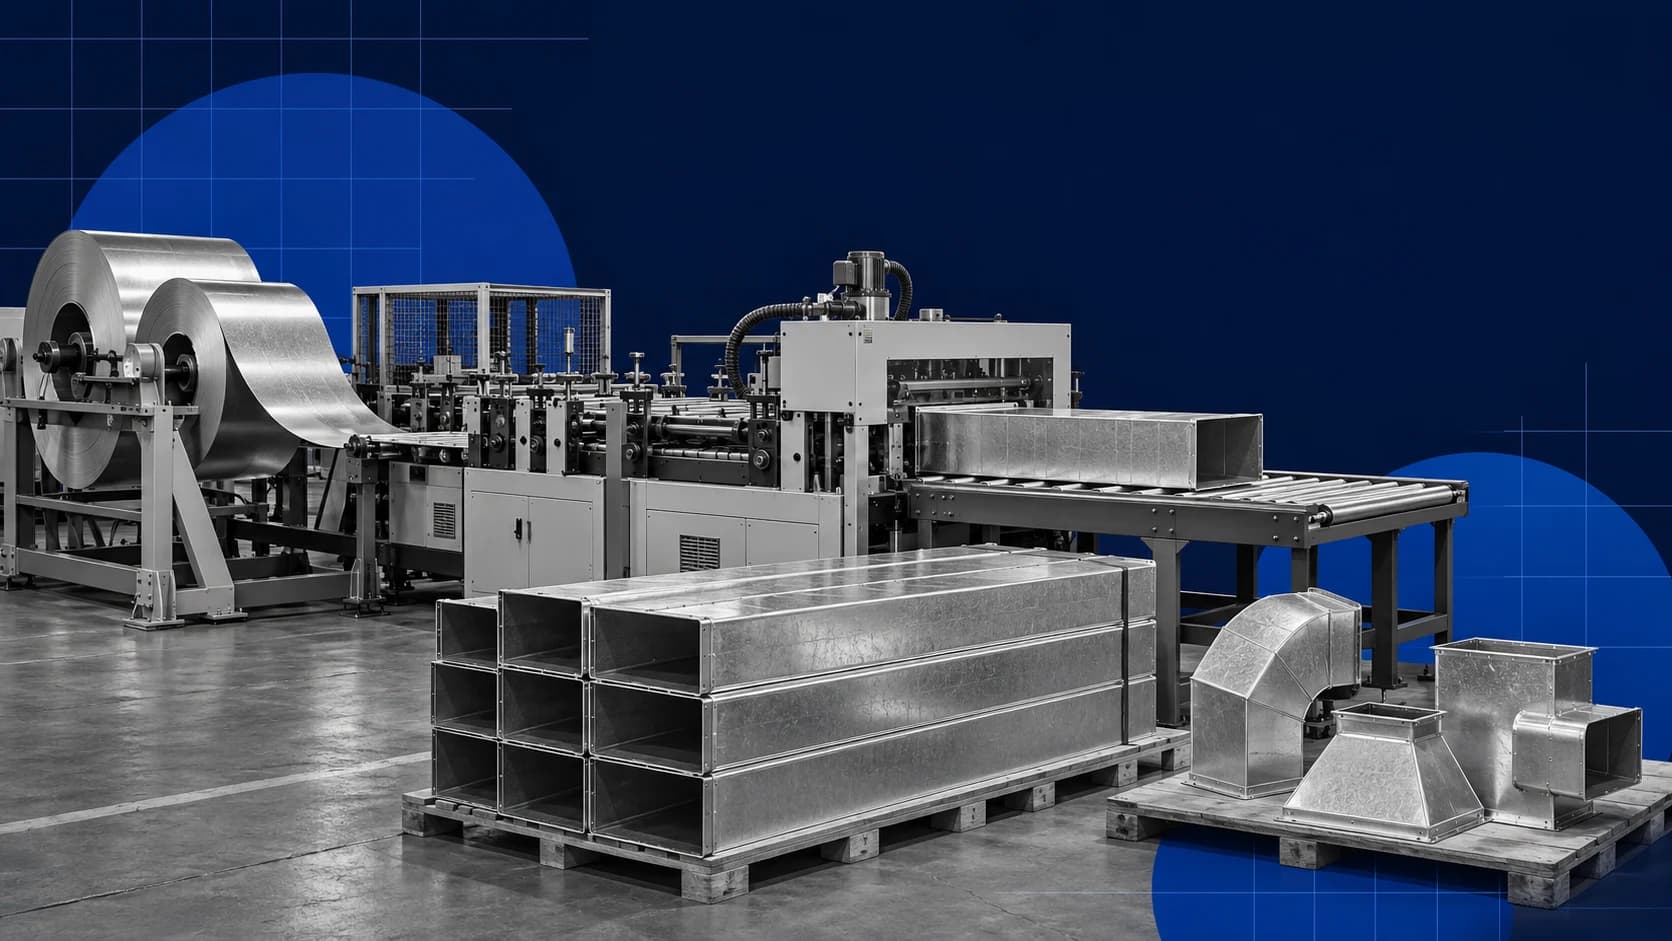
Consider a shop making ductwork for several construction projects. One delivery may require straight sections, elbows, transitions, and accessories in different sizes and materials. A coil line may produce the straight work while fittings follow a separate cutting, forming, and assembly route.
The production plan must connect those routes to the complete delivery, not just the output of one machine. A finished stack of straight duct cannot complete a package that is waiting for a fitting. Pieces also need identification that links them to the project, drawing revision, and delivery sequence.
The shop order carries more than a quantity. Depending on the job, it may specify dimensions, material and thickness, connection details, pressure class, reinforcement, lining, and required inspection. These determine which material can be used and which operations each piece needs. The project specification and applicable standards govern the work; the route and approvals vary by shop.
A customer’s requested date also needs a clear meaning. Is it collection from the shop, delivery to the site, or availability for a particular installation sequence? Confirm the receiving location, unloading constraints, and whether the site can use a partial package. An inquiry or preliminary drawing may support estimating; it is not necessarily authorization to fabricate.
Before committing a date, the team needs answers to a few questions:
If a supplier changes its date, the buyer and planner can identify the affected jobs, check approved alternatives, and resequence work. The account owner can then give the customer a useful update: what is affected, what options are available, and when the next decision will be made.
MEP Academy’s guide to sheet-metal fabrication describes the drawing and shop-order details behind this work. The exact routing and approvals depend on the shop and project.
A planner may group work by material, thickness, or machine setup to reduce changeovers. The customer may need a smaller set of pieces for a particular area first. The best sequence balances both needs: a machine can be busy while the parts required for the next installation are still waiting in another queue.
Check the approved drawing revision and the required material, dimensions, connections, and inspection requirements. If a revision arrives after release, identify which pieces have not started, which are in process, and which are finished. Hold affected work until the change is understood, then agree on any effect on cost or delivery.
A purchase order sent is not the same as material confirmed or received. For critical sheet, components, or consumables, the buyer needs the specification, required quantity, supplier, confirmed date, and the job that needs them. Check stock that is usable and available for that order; material already allocated elsewhere cannot be promised twice.
Work backwards from when the material is needed at the operation, allowing time for receipt and any required inspection. If a delivery slips, check which jobs reach that constraint first. A partial receipt, an approved substitute, or a different sequence may help; technical and customer approvals still govern substitutions.
MRP starts with a requirement, then offsets the required receipt by the time needed to obtain it. A simplified example for one specification of coil:
| Input | Quantity |
|---|---|
| Coil required for released packages | 900 m |
| Usable, unallocated stock | 240 m |
| Confirmed, unallocated receipt due before production | 300 m |
| Stock the shop intends to protect | 60 m |
| Net requirement | 420 m |
The calculation is 900 + 60 − 240 − 300 = 420 m. If the supplier's minimum order is 500 m, the planned order becomes 500 m. If the 300 m receipt is late or belongs to another job, the shortfall changes. The planned balance is only as reliable as its inventory, allocation, and supplier-date inputs.
Suppose the coil must be ready at the line next Friday. If receiving and inspection require one working day, it needs to arrive by Thursday. With a confirmed five-working-day lead time and no holidays, the buyer would need to place the order by the preceding Thursday. Confirm the actual lead time and receipt date with the supplier; the calculation does not reserve material or create a supplier commitment on its own. Technical approval still governs any substitute.
A feasible total for the week can hide an overloaded work center. Suppose three released packages require 12, 9, and 8 hours at the fitting assembly bench, including their expected setups. The load is 29 hours. If two qualified assemblers provide 32 available labor hours after breaks and planned absences, the bench has three hours of remaining capacity for that period. This simplified check assumes the work can be divided between the two people; a task requiring both at once needs a different calculation.
Now check when the hours are needed. If 21 hours must finish by Wednesday but only 16 qualified labor hours are available by then, the week is feasible in total and still misses the intermediate date. The planner can split an agreed delivery, move work to an approved alternate route, arrange qualified overtime, or negotiate a new date. Each option needs a check on material, quality, cost, and other commitments.
Sequence the constraint with due dates and changeovers in view. Grouping similar gauges may save setup time; grouping everything by gauge may leave a customer waiting for one fitting. Release only enough ready work to support the next operations. A large queue can make the floor look busy while increasing the time a critical package waits.
Once work is released, control compares the plan with actual progress and makes exceptions visible early enough to act. The team needs the current operation, completed and rejected quantities, work waiting between steps, material status, and the next required date—not just a list of jobs marked open.
For each exception, identify the affected order and constraint, the likely impact on downstream work and delivery, the person responsible, and the next update. A late coil delivery might call for a supplier escalation and a revised sequence; a machine stop might require maintenance, an alternate route, or a new capacity commitment. Check the effect on other jobs before making the change.
A practical control board can show the promised date, planned next operation, current status, quantity complete, blocking issue, owner, and next update for each critical package. Compare the same milestones at the same review time. If a job is behind, distinguish time already lost from the latest credible recovery estimate; the team needs both to decide what moves next.
Protect near-term work from unnecessary changes while keeping a deliberate path for genuine emergencies. When priorities change, update the dispatch list and tell the operator, buyer, maintenance team, and account owner as appropriate. Compare the recovery plan with actual progress until the affected delivery is complete.
Rush work is part of serving customers. The key is knowing what it displaces before promising a date.
Imagine a constrained operation has two jobs scheduled:
| Work | Fabrication | Inspection | Collection |
|---|---|---|---|
| Project A | 08:00–12:00 | 12:00–13:00 | 14:00 |
| Project B | 12:00–15:00 | 15:00–16:00 | 17:00 |
An urgent job arrives. It needs two hours on the same operation, one hour of inspection, and collection at 11:30. If it runs first, Project A finishes inspection at 15:00 and Project B at 18:00. Both existing collection slots are missed unless the team changes the plan.
Before accepting, confirm the rush order is released and its material is available. Then compare a partial delivery, another qualified route, additional capacity, or a revised sequence. Check the effect on each customer and the receiving site, not just the machine schedule.
This is a fictional example, but the decision is familiar: an urgent order may be worth taking; the rest of the schedule still needs an owner and a recovery plan.
Capacity can mean several different things. Theoretical capacity is the ceiling at the ideal rate; demonstrated capacity is what comparable work has actually achieved over a defined period. To assess a new order, start with a realistic capacity estimate and account for work already committed on the relevant resources. Historical averages need adjustment when the product mix, staffing, or shift pattern changes.
A machine’s rated speed does not account for maintenance, changeovers, stops, slow running, or rejected work. Estimate good output using a consistent time boundary:
Planned run time × ideal rate × availability × performance × quality
= estimated good output
Check capacity at two levels. A rough-cut check asks whether the master schedule fits the key resources by week. A detailed check loads individual operations into available shifts, including setup, labor, and existing work. The first identifies a likely overload; the second shows whether the sequence can meet individual due dates.
For a repeat batch on a fictional duct line:
| Input | Assumption |
|---|---|
| Scheduled line time | 40 hours |
| Maintenance and changeovers | 5 hours |
| Planned run time | 35 hours |
| Ideal rate for the selected component | 12.5 pieces per hour |
| Availability | 80% |
| Performance | 90% |
| First-pass quality | 300 accepted pieces out of 315 produced |
The line is expected to run for 28 hours, produce 315 pieces, and pass 300 pieces on the first inspection. If the order requires 330 accepted pieces, the plan is short by 30. At the same assumed rate and loss factors, closing the gap requires approximately 3.5 additional planned run hours.
That is an estimate for one operation, not a completed delivery. The team still needs to check material, labor, downstream work, inspection, and transport. For mixed products, use the correct rate for each product. If maintenance or setup time has already been removed from planned run time, do not subtract the same loss again in the availability factor.
Overall equipment effectiveness (OEE) combines three factors for a defined asset and period:
| Factor | Calculation | What it reveals |
|---|---|---|
| Availability | Operating time ÷ planned production time | Time lost to stops |
| Performance | Ideal cycle time × total output ÷ operating time | Losses from slow running and small stops |
| Quality | First-pass good units ÷ total units | Output that needs rework or is rejected |
For the example above, OEE is 80% × 90% × (300 ÷ 315) = approximately 68.6%. The maintenance and changeover windows were excluded before calculating planned run time.
The factors point to different investigations. A drop in availability may call for a review of stop duration and reasons. A performance loss calls for a comparison of actual operating speed with the correct product rate. A quality loss calls for first-pass acceptance and the reasons for rejection or rework. These distinctions help planners revise capacity assumptions and help operations find the underlying issue.
A machine may stop while waiting for material or run slowly because of a process issue. Break the result down by job, time, and loss category so the right team can investigate.
Agree on the asset boundary, planned time, ideal rate, and quality rules before comparing results. NIST notes that OEE definitions vary; consistent definitions matter more than a generic target.
In a high-mix shop, a count of large duct sections is not interchangeable with the same count of small fittings. Use an appropriate ideal cycle time for each product and weight mixed-product calculations consistently. OEE measures an equipment boundary; it does not tell you whether the full project package has passed inspection or reached the customer.
Machine run and stop signals, production counts, and quality results can help explain the score. A machine signal may show that a stop occurred without showing why. Agree on stop categories, align timestamps, and give operators a way to add the missing reason. Review missing or inconsistent data before treating it as a reliable loss.
Production needs to know when equipment will be unavailable. Maintenance needs time, people, parts, and the correct procedure to do the work. Review both schedules together before the week begins.
When a machine stops, record the asset, time, symptom, and next update. The planner can assess the affected jobs while maintenance diagnoses the problem. If a replacement part is needed, purchasing can confirm availability and the account team can communicate realistic options to customers.
Keep machine downtime separate from technician labor. Downtime may include waiting for a part or access; labor is the time people spend on the repair. Both matter, but they answer different questions.
Condition measurements such as vibration can provide additional context for rotating equipment. A change should be assessed against the machine’s baseline, measurement location, speed, and operating load. It is a reason to investigate, not proof of a particular fault or an exact failure date.
Suppose a technician observes a sustained change in vibration on a duct line's drive motor. After inspection, the team determines that follow-up repair is needed. The decision to continue, restrict, or stop operation follows the plant's safety procedures and the actual condition of the asset.
If a replacement part is not in the storeroom, maintenance confirms the part specification and purchasing checks supplier availability. The planner identifies the jobs that need the line and the latest useful arrival time. The account owner can then discuss a partial delivery, alternative sequence, or revised date with affected customers.
A supplier's estimated arrival is one input to the recovery plan. Allow for receiving the part, repair, checks, and return to service before committing to production time. Record what was found and what work was completed so the next team has a useful history. This example is illustrative; it does not assume a sensor can diagnose a fault or predict its failure date.
A short review can connect the schedule to the decisions that matter:
Track schedule adherence and complete deliveries alongside downtime and OEE. A productive machine is valuable when the right work reaches the customer.
| Measure | Example definition | What to investigate |
|---|---|---|
| Schedule adherence | Jobs completed by their scheduled date and quantity ÷ jobs scheduled for completion | Whether the production plan was met |
| On-time, complete delivery | Packages received by the agreed date with all agreed pieces ÷ packages due | Whether the customer got the complete commitment |
| Throughput | Accepted output ÷ elapsed time for the chosen operation | How much good work the process delivered |
| Work in process | Partly completed work within a defined boundary, plus its queue age | Where work is accumulating or stalled |
| Planned and unplanned downtime | Hours in each agreed category for the asset and period | Which interruptions were expected and why others occurred |
| Maintenance schedule compliance | Scheduled maintenance jobs completed in the agreed period ÷ jobs on the agreed schedule | Whether the equipment work was carried out as planned |
| Supplier delivery reliability | Purchase-order lines received by the confirmed date and quantity ÷ lines due | Whether a material commitment arrived as planned |
Define the period, population, exclusions, and treatment of partial deliveries before comparing results. For example, 18 of 20 scheduled jobs completed on time and in quantity gives 90% schedule adherence. That does not establish 90% on-time customer delivery: the two overdue jobs may belong to one critical package, or a completed package may still be awaiting collection. Distinguish supplier delay from an order the shop placed late.
Use the measures together. High throughput alongside rising work in process can mean upstream work is arriving faster than a downstream constraint can process it. A strong OEE score can coexist with incomplete packages if the line made the wrong mix. Review the actual jobs and queues behind each number before changing targets.
PPC is the planning and control process; different systems can support different parts of it. Their responsibilities vary by plant.
| System or method | What it contributes to the plan |
|---|---|
| Enterprise resource planning (ERP) | Orders, purchasing, inventory, and other business records; it may also support master scheduling and MRP |
| MRP | Time-phased material requirements based on demand, bills of materials, inventory, and lead times |
| Manufacturing execution system (MES) | Production execution information, such as operation status, counts, and shop-floor activity |
| Computerized maintenance management system (CMMS) | Maintenance work orders, asset history, planned work, and equipment windows |
| OEE | A view of availability, performance, and quality losses for a defined equipment boundary |
A system can provide a record or calculation, but the plan still depends on people confirming the inputs and agreeing how to respond to exceptions.
Planning establishes the products, resources, and timing. Control monitors execution and coordinates adjustments when conditions change.
OEE can help estimate good output when its factors apply to the product and period. Check materials, labor, mix, downstream constraints, and the time boundary before treating it as a delivery commitment.
Planned maintenance consumes an agreed equipment window; unexpected failures can interrupt the schedule. Sharing upcoming work, equipment status, and repair updates helps production account for constraints and make recovery decisions.
Canary is building an OEE platform to connect the production plan with what happens on the floor. The aim is to give production and maintenance teams a shared view of the equipment losses that affect a job and the work needed to address them.
The platform is being developed around a practical workflow:
These OEE and equipment-monitoring capabilities are in development; availability, data connections, and scope depend on the eventual implementation. Today, Canary helps teams organize maintenance work with work orders linked to assets, assignees, schedules, planned parts, and procedures.
If your team is working through production visibility, OEE, or maintenance coordination, we would like to understand your operation and show you what Canary is building.
Keep exploring
Canary OEE · In development